Mobility Scooter Frame Fatigue and Load Cycle Testing
A mobility scooter is only as dependable as the structure that carries the user, the battery pack, and the road. For importers, DME dealers, and brand owners, frame fatigue and load cycle testing is the quiet discipline that separates a product that survives three years of daily service from one that develops cracks in the first season. This article explains how frame fatigue is validated, where frames usually fail, how test conditions are defined, and how buyers can write fatigue requirements into a purchasing specification.
Why the Frame Must Be Fatigue Validated
A frame does not fail because of one large event. It fails because of thousands of small ones. Every time a user steps on and off the platform, rolls over a curb, brakes hard at a junction, or leans into a turn, the welded structure absorbs a load cycle. None of these individual events is enough to break the steel or aluminium on its own, but the accumulation of micro-damage at stress concentrations is what engineers call cumulative damage. Over months and years, a crack that starts at a weld toe grows until it reaches a critical length, and the component loses its load path.
Daily cyclic loading is unavoidable. Getting on and off the scooter places an asymmetric vertical load through the floor pan. Crossing a threshold or a dropped kerb produces a sharp impact that sends a moment into the front fork and the steering column. A sudden stop transfers inertia from the seated mass into the seat post and the chassis. Each of these is a repeatable event, and repeatability is exactly what makes it a fatigue problem rather than a one-off overload problem. A static strength check alone cannot catch this, because a frame that passes a single maximum-load proof test can still fail after a realistic number of ordinary cycles.
The cost of ignoring fatigue shows up downstream. A structural failure in the field means a warranty claim, a returned unit, a safety incident report, and reputational damage with the distributor or the DME channel. Validating the frame before mass production is far cheaper than recalling it after.
How the Load Spectrum Is Derived
The first step in any fatigue program is turning real usage into a test input. You cannot validate a frame against a number you invented; you validate it against a load spectrum that represents how the product is actually used. The spectrum is built from several field inputs rather than a single fixed figure.
Body mass distribution matters because the user’s weight is not a point load. It sits on the seat, transfers through the seat post, and the feet may add load to the floor. Carrying capacity class defines the design envelope: a standard scooter, a heavy-duty bariatric unit, and a travel folding model each carry a different maximum and a different typical load. Road grade classification sets the roughness and the obstacle height the frame is expected to meet, from smooth indoor flooring to cracked pavements and ramp transitions. Average daily trip count and daily operating hours translate usage intensity into a cycle budget over the product’s intended service life.
The method is to record representative field conditions, bin them into load levels of varying magnitude and frequency, and reconstruct a representative mission profile. That profile becomes the basis for both the cyclic test and the accelerated variant. Engineers often plot the resulting stress against cycle count on an S-N curve to estimate life and to set the test target. The key is traceability: every load level in the test should map back to a measured or declared use case, not to an arbitrary assumption.
Typical Failure Points on a Mobility Scooter Frame
Fatigue does not strike uniformly. It concentrates at geometry changes, welds, and moving interfaces. The locations below are the usual suspects during teardown and field returns:
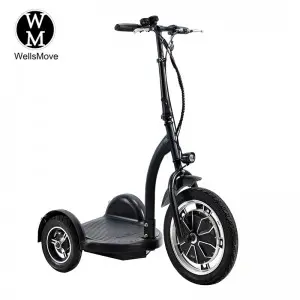
- The steering head tube and the junction where the upright meets the front fork crown, because steering inputs and road shock enter here.
- The seat post root, where the entire seated mass pivots and the cross-section changes abruptly.
- The chassis cross members, which bridge the left and right rails and carry bending from kerb strikes.
- The battery tray suspension points, which see both static weight and vibration from the road.
- The folding mechanism latch, a stress raiser that opens and closes and must hold under load.
- The front fork, which takes vertical impact and braking reaction on every ride.
Each of these points should receive targeted strain gauging during development so the test plan stresses the right location with the right magnitude.
Comparing the Test Types
Frame validation is not a single test. Different test types answer different questions, and a complete program combines several of them.
Static strength and overload testing verifies that the frame holds a defined multiple of the rated load without permanent deformation. It proves the margin above normal use but says nothing about long-term cycling. Fatigue cycling testing applies repeated loads below the ultimate strength to find the life to crack initiation and the life to functional failure. Drop and impact testing checks the response to a single severe event such as a kerb drop or a fall from a low height. Twist and single-wheel obstacle testing loads the frame in a non-symmetric way to simulate one wheel climbing a step while the other stays down. Vibration testing reproduces the random spectrum of road input to assess both structural response and component loosening over time.
Used together, these tests cover overload, cyclic life, impact, asymmetry, and resonance. A buyer should ask which of these the supplier actually performs rather than assuming one static check is sufficient.
Setting the Test Conditions
A fatigue test is only meaningful if its conditions are defined and repeatable. The load magnitude and direction must reflect the real force path: vertical through the seat, lateral through the handlebar, fore-aft through braking. The number of cycles should represent the intended service life converted through the load spectrum, not a round number chosen for convenience. Frequency is a practical compromise; it must be high enough to finish the test in a reasonable window yet low enough that the material does not heat or that the fixture dynamics change the stress state.
Fixturing and constraint method decide whether the test measures the frame or the rig. The frame should be supported at realistic reaction points, with the same freedom of movement the real scooter has, so that loads enter the structure the way they do in use. The failure criterion must be written before the test starts. Common criteria include a crack length measured at the weld toe, a permanent deformation beyond a set limit, or a functional failure such as the loss of steering or a broken load path. Agreeing the criterion in advance prevents argument over whether a result passed.
Accelerated Testing and Correlation
Because real-life cycling can mean hundreds of thousands of repetitions, laboratories use accelerated testing to compress time. This is useful but dangerous if misapplied. Raising the load amplitude, increasing frequency, or removing rest periods can change the failure mode so the accelerated test no longer represents the field. A weld that fails by overload in a high-load accelerated run may have failed by corrosion-assisted cracking in the field, and the two are not interchangeable.
Tip: Treat any acceleration factor as a hypothesis that must be validated against field return data, not as a license to multiply the load until the test finishes by Friday.
The disciplined approach is to run a correlation study: perform an accelerated test, then confirm the failure location and failure mechanism match what is seen in service or in a slower baseline test. Only then is the acceleration factor accepted, and even then it should carry limits. Do not extrapolate beyond the validated range, do not change two acceleration variables at once, and document the assumptions so a third party can reproduce the result. When correlation data are absent, the conservative path is a lower acceleration factor with a wider safety margin.
Welding and Manufacturing Consistency
Fatigue life is decided as much on the factory floor as in the engineering office. A frame with a perfect drawing can still fail if the welds are inconsistent. Weld class and acceptance level should be specified, with particular attention to the root and the weld toe where cracks begin. Post-weld treatment such as grinding the toe or shot peening can improve life by reducing stress concentration, and the process should be controlled rather than optional.
Tooling and fixture location keep every unit identical. A jig that drifts by a few millimetres changes the joint geometry and therefore the fatigue result from one batch to the next. Sampling and sectioning are the only ways to be sure the production weld matches the validated sample. Cutting a finished joint, etching it, and inspecting the penetration and lack-of-fusion is unglamorous but it is what keeps the claimed fatigue life honest across a production run.
Correspondence with Standards
Frame testing should be mapped to the applicable standard and to the buyer’s own specification. Different markets and different product classes reference different documents, and the correct document depends on where the scooter is sold and how it is classified. Where a requirement is unclear or where the standard is revised, the safe wording is that the detail is subject to the latest standard text and official notices. Buyers and suppliers should agree which edition of the standard applies and record it in the contract, because testing to an outdated edition creates a compliance gap that only appears during an audit or a market surveillance check.
Writing Fatigue Requirements into the Specification
For a purchasing team, the value of this discipline is that it can be written down. A strong specification turns fatigue from a vague hope into an acceptance clause. The prototype quantity should be stated: typically more than one sample so that a single good or bad result is not taken as proof. The test report content should be defined in advance, listing the load spectrum, cycle count, frequency, fixture description, strain gauge map, observed failure location, and the pass or fail against the agreed criterion.
Batch production sampling keeps the claim alive after the first run. A defined number of units per batch should be pull-tested or at least proof-loaded, with the result logged. Retained samples and re-inspection let a buyer reopen a question if field returns suggest a drift in quality, and they give leverage during a supplier audit. The specification should also state what happens on failure: re-validation, corrective action, and re-testing before further shipments.
FAQ
Does a passed static load test mean the frame is fatigue safe?
No. A static test confirms the frame holds a peak load once. Fatigue life depends on repeated lower loads, which a static test does not measure.
How many cycles should a mobility scooter frame survive?
The cycle target should come from the declared service life and the load spectrum, not from a fixed industry number. The method is to convert intended daily use into total cycles over the product life.
Is accelerated fatigue testing reliable?
Only when the acceleration factor is correlated to field or baseline data. Without correlation, accelerated results can misrepresent the real failure mode.
Where do mobility scooter frames usually crack first?
Most often at welds and geometry changes: steering head, seat post root, chassis cross member, battery tray point, folding latch, and front fork.
What weld checks prove production consistency?
Defined weld class, controlled post-weld treatment, stable tooling, and periodic sectioning of finished joints to verify penetration and lack of fusion.
Related Pages
- Mobility Scooter Wholesale: Complete Buyer’s Guide 2026
- CE Certification for Mobility Scooters: Complete Guide
- How to Get the Best Price on Mobility Scooters
- Mobility Scooter Factory Audit Guide
Post time: Oct-30-2026